Case Study • Engineering Case Study
Industrial Control Panel Design & Multi-Zone PID Temperature Control for Extruder Cylinder
Complete electrical panel engineering complying with IEC 61439, Siemens PLC programming, and implementation of closed-loop Split-Range PID temperature control across 5 heating/cooling zones of a polymer extruder cylinder and die.
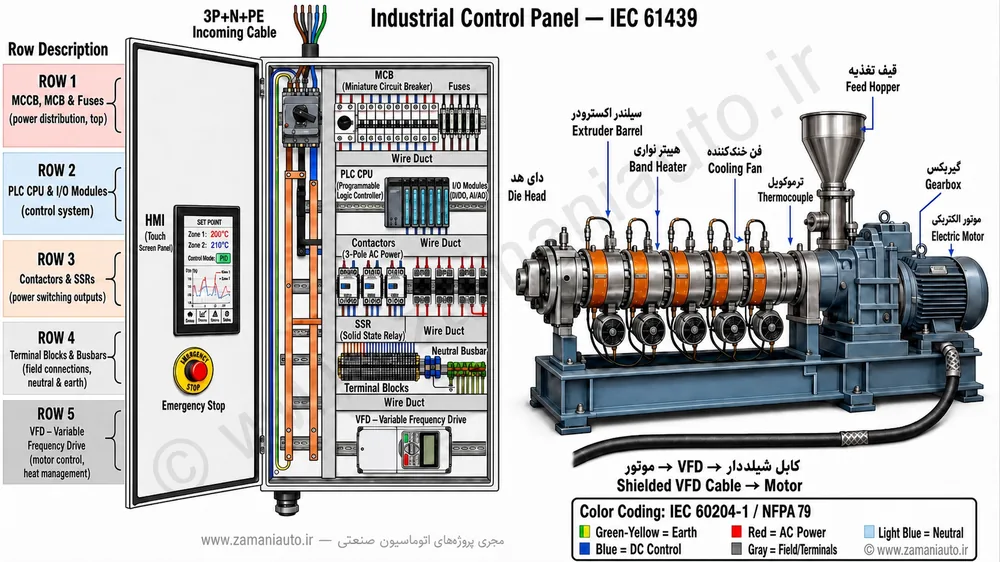
📷 Project Documentation
🎯 Challenge
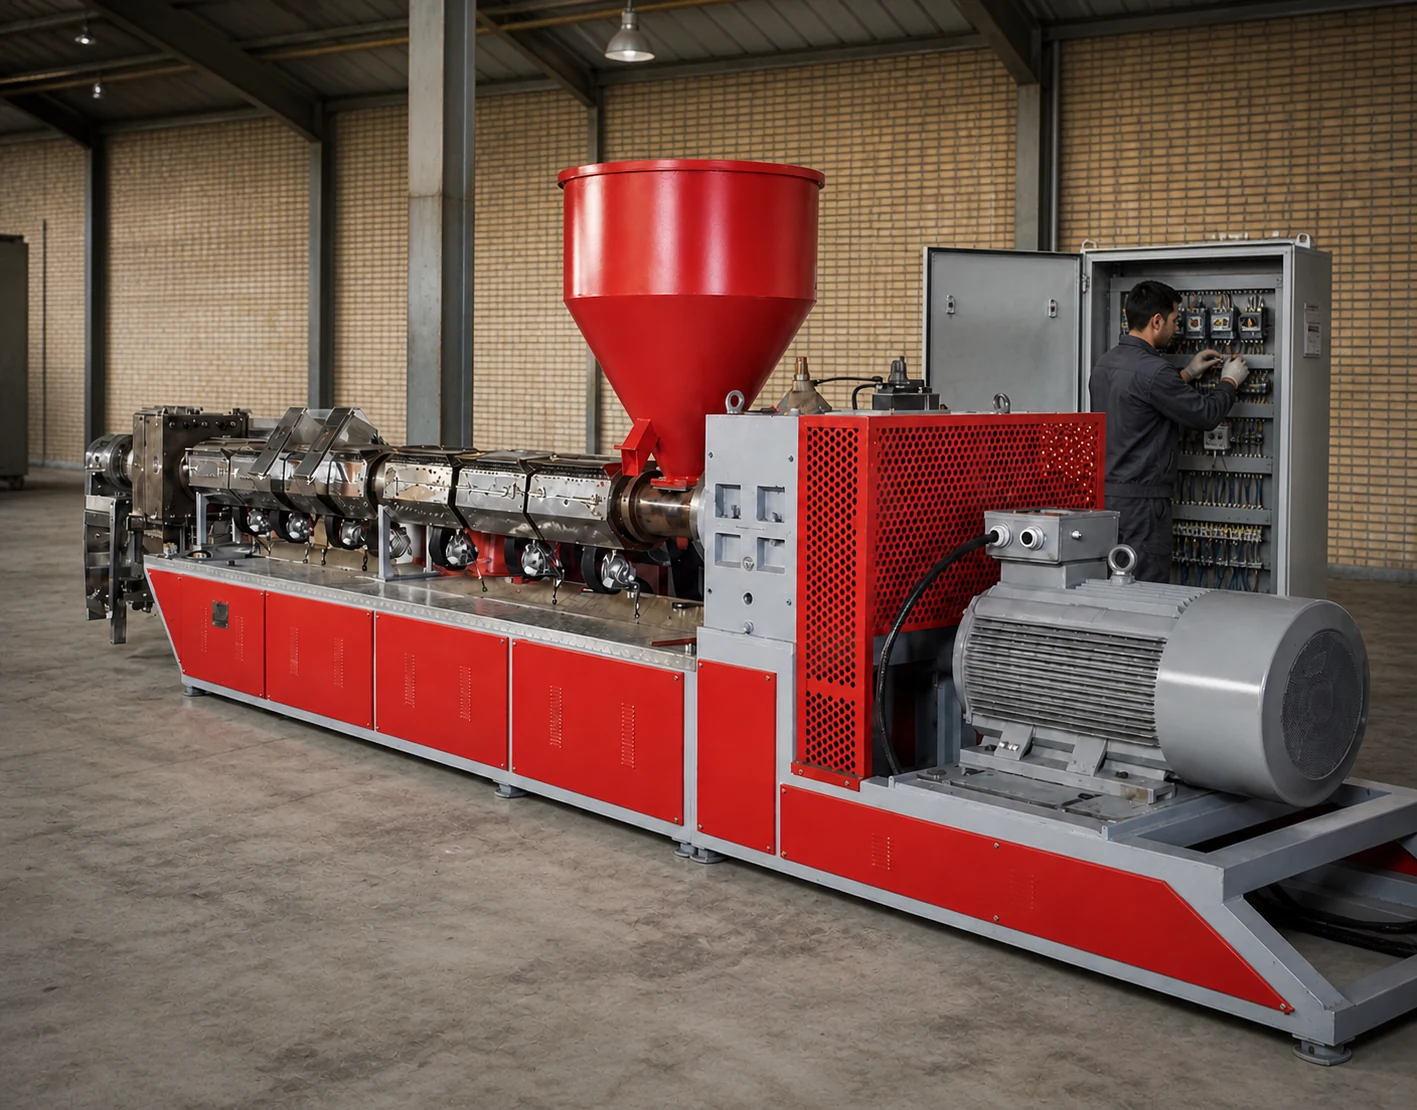
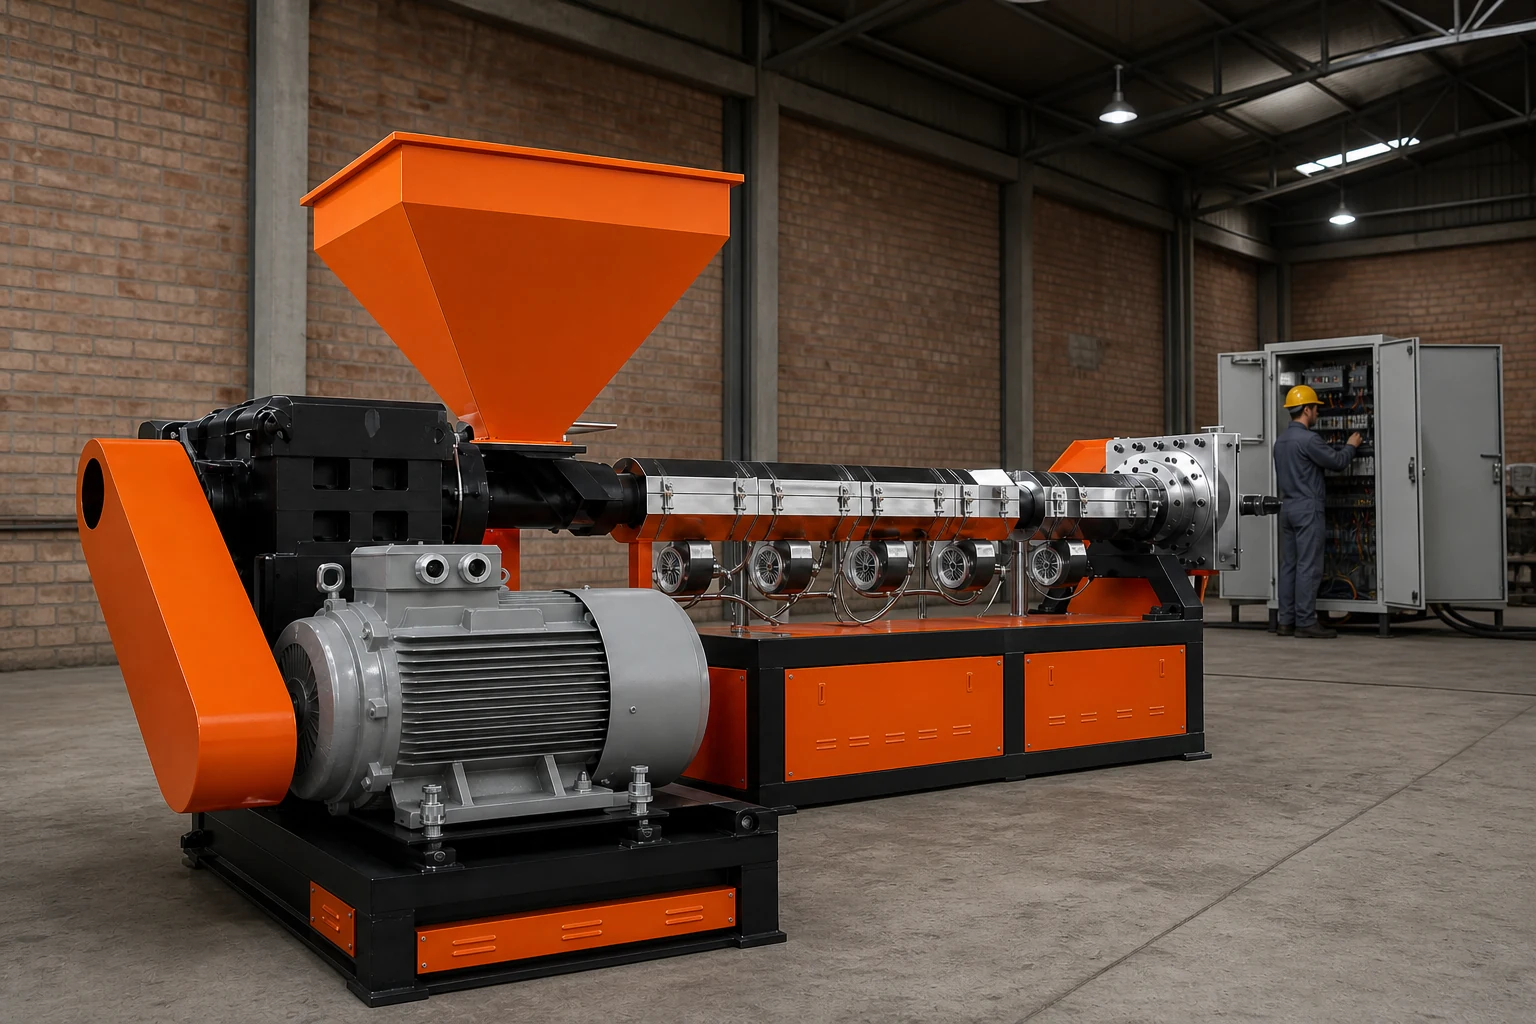
In polymer extrusion, barrel temperature directly determines melt rheology, Melt Flow Index (MFI), profile dimensional consistency, and prevents thermal degradation. Key engineering challenges included:
• Severe cross-zone thermal coupling via the solid steel barrel body.
• Non-linear exothermic shear heating generated by screw rotation at high RPM causing persistent temperature overshoot.
• Asymmetric heating/cooling dynamics (rapid ceramic band heaters vs. sluggish air-blower cooling delay).
• Obsolete electrical control cabinet, high EMI noise corrupting thermocouple millivolt signals, and frequent mechanical contactor failures.
🔧 Solution
To achieve deterministic temperature regulation, the following engineering methodology was deployed:
1. Industrial Control Cabinet Engineering:
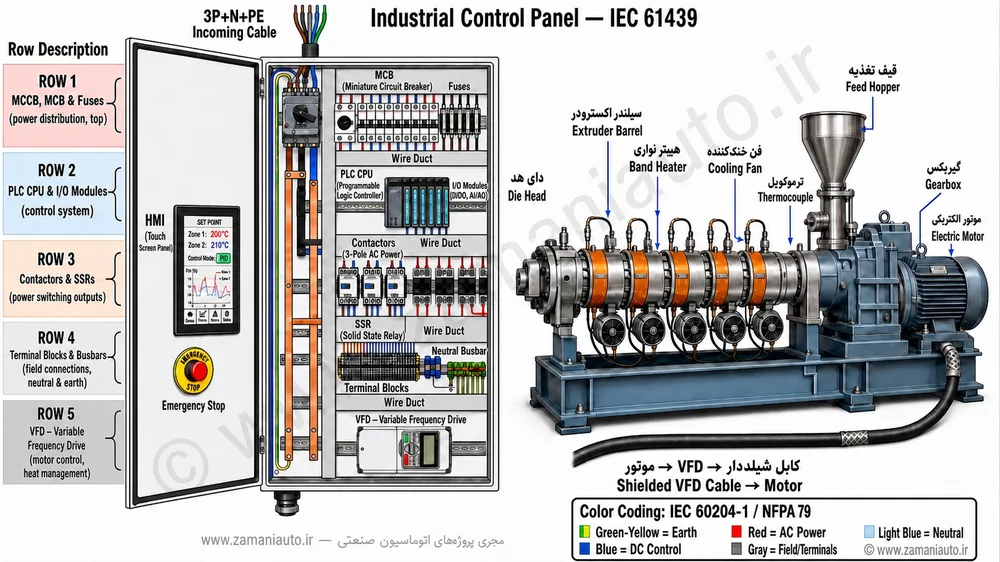
Electrical schematics developed in EPLAN Electric P8 conforming to IEC 61439-2 and IEC 60204-1. Segregated power and instrument wiring ducts, industrial Solid State Relays (SSRs) mounted on heavy-duty heatsinks for high-frequency PWM switching, and robust EMC grounding architecture.
2. Advanced Multi-Zone Split-Range PID Control:
Siemens PLC programmed via TIA Portal in IEC 61131-3 SCL. Configured closed-loop PID_Temp algorithms featuring dual Split-Range outputs: 0 to 100% modulating heater power via Pulse Width Modulation (PWM), and 0 to -50% engaging cooling blowers with an optimized deadband to prevent simultaneous heating/cooling chatter and energy waste.
3. System Tuning & Feedforward Compensation:
Pretuning and Fine-tuning cycles executed to identify thermal process time constants and delay parameters. Implemented feedforward compensation tied to screw extruder drive (VFD) velocity to proactively counter mechanical shear heat generation.
4. High-Performance HMI & Functional Safety:
HMI visualization designed per ISA-101 guidelines with prioritized alarms (HH, H, L, LL), real-time process curve trending, thermocouple break detection, and Category 3 hardware safety interlocks.
Recorded technologies and equipment
Siemens S7-1200 PLCTIA Portal V17 (SCL)Siemens KTP700 Basic HMISplit-Range PID_TempIndustrial SSR (Zero-Cross)Fe-CuNi Type J ThermocouplesEPLAN Electric P8IEC 61439-2 StandardIEC 60204-1 Safety